NatureFlow Ventures provides innovative water treatment solutions with top-tier technology and service, specializing in water and wastewater treatment since 2023.
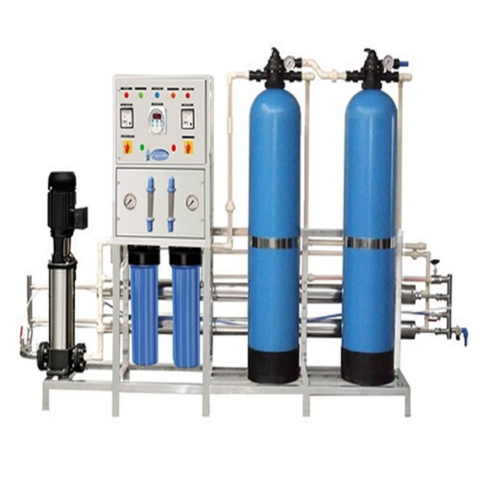
Water is the silent worker in every industry. Whether you run a boiler, a pharmaceutical lab, or a food processing unit, the quality of your water directly impacts your product, equipment, and operational efficiency. At Nature Flow Ventures, we design and deliver reverse osmosis system industrial solutions that transform ordinary tap or borewell water into a reliable, high-purity resource. We are not just manufacturers; we are trusted partners who understand that every drop matters.
Have you ever dealt with scaling on pipes, corrosion in boilers, or inconsistent product quality? These are often signs of untreated water. Dissolved salts, silica, bacteria, and heavy metals silently reduce your efficiency and damage your systems. A properly designed reverse osmosis system industrial removes up to 99% of contaminants, delivering water you can trust.
The result? Lower maintenance costs, extended equipment lifespan, and a high-quality final product that consistently meets industry standards.
Let us simplify the science. Your feed water first passes through pre-filters to remove suspended solids and chlorine. Next, a high-pressure pump pushes the water through a specially designed semi-permeable membrane.
Clean water, known as permeate, moves through for industrial use, while concentrated salts and impurities, called reject water, are safely drained or recycled. This process is simple, efficient, and energy-saving.
At Nature Flow Ventures, we customize every reverse osmosis system industrial according to your raw water quality and purification requirements.
| Parameter | Specification Range |
|---|---|
| Flow Rate Capacity | 250 LPH to 50,000 LPH (Customizable) |
| Membrane Type | Thin Film Composite (TFC) – Dow / Hydranautics / Vontron |
| Recovery Rate | Up to 75% (Higher with recycle) |
| Salt Rejection | 97% to 99.5% (Single Pass) |
| Feed Water TDS | Up to 10,000 ppm (with antiscalant) |
| Pre-treatment | Multi-media Filter + Activated Carbon Filter + Antiscalant Dosing |
| Post-treatment | UV Sterilizer / Ozonator (Optional) |
| Control Panel | Manual to Fully Automatic (PLC/SCADA Based) |
| Material of Construction | FRP / Stainless Steel 304 / SS 316 for High Purity |
| Power Supply | 415V, 3-Phase, 50Hz |
| Skid Mounted | Yes – Compact Footprint for Easy Installation |
Higher capacity or ultra-pure water versions can include double-pass RO systems, mixed bed polishers, or EDI (Electro-Deionization) as additional purification stages.
Every industry has unique water treatment needs. A textile dye house requires different purification standards compared to a beverage manufacturing unit. That is why we never provide a one-size-fits-all reverse osmosis system industrial.
Our process begins with a free consultation and detailed water sample analysis. We carefully understand your daily water consumption, installation space, and budget before designing a system tailored to your requirements.
From manufacturing to installation, commissioning, and staff training, our support continues throughout the journey. Our Annual Maintenance Contracts (AMC) ensure your system runs efficiently for years.
Choosing a Nature Flow Ventures reverse osmosis system industrial means eliminating frequent boiler cleaning, reducing product rejection rates, and maintaining regulatory compliance.
Do not let poor water quality limit your industrial growth. Whether you need a small skid-mounted unit or a large custom-built industrial RO plant, Nature Flow Ventures is ready to support your water purification journey.
Contact us today for a no-obligation consultation and water analysis. Let us transform your water challenges into a story of pure success.

